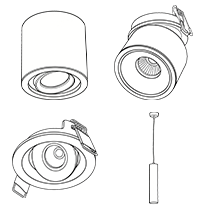
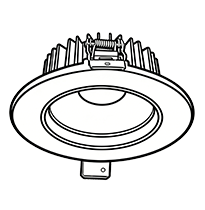
LED Down Light save your time & money
Explore the LED Down Light series
Expansive Utility, Igniting A World Of Innovation
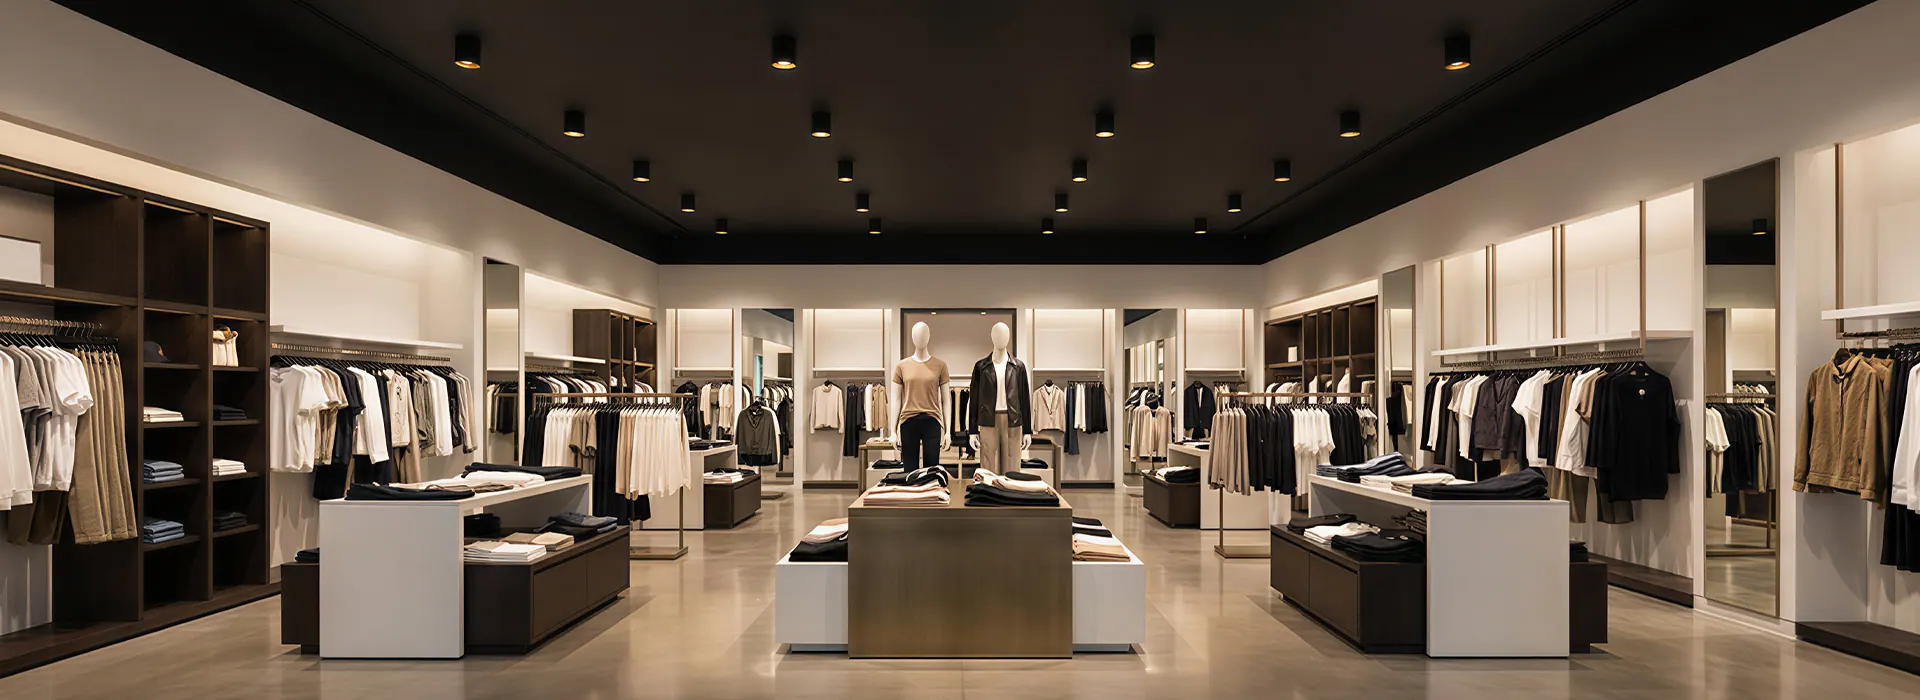
Large Clothing Store Lighting Solutions
Ceiling downlights with precise beam angle and color temperature adjustment create vibrant and prominent clothing display areas, enhancing customer interest in trying on clothes and boosting sales conversion.
Explore More Solutions
Restaurant Ambient Lighting Solutions
Ceiling downlights with soft dimming design reduce glare, creating a warm and romantic dining environment that promotes relaxation and social interaction among guests.
Explore More Solutions

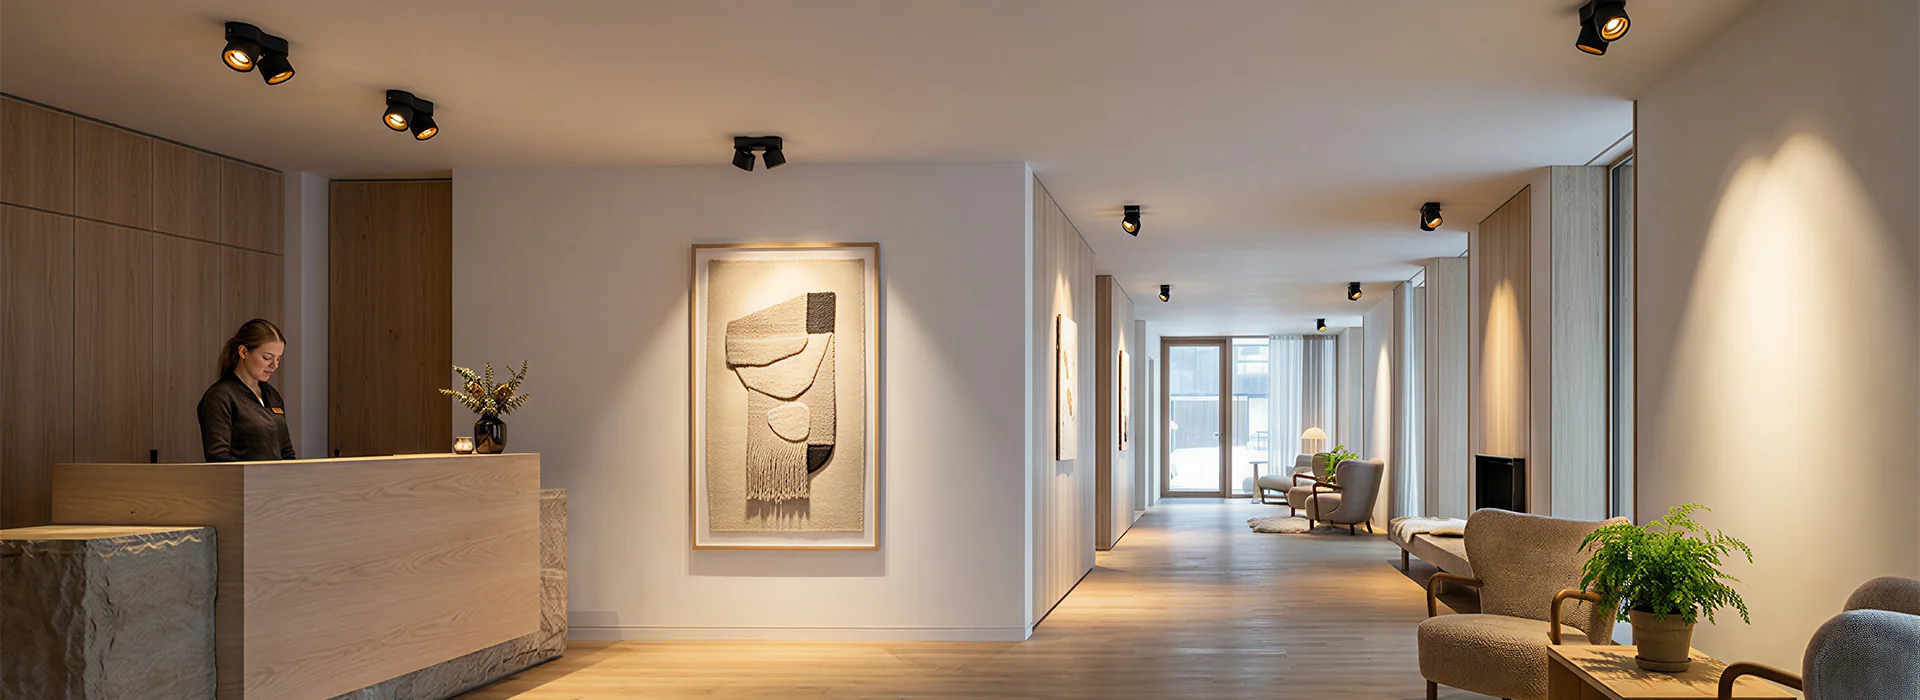
Hotel Lobby Reception Lighting Solutions
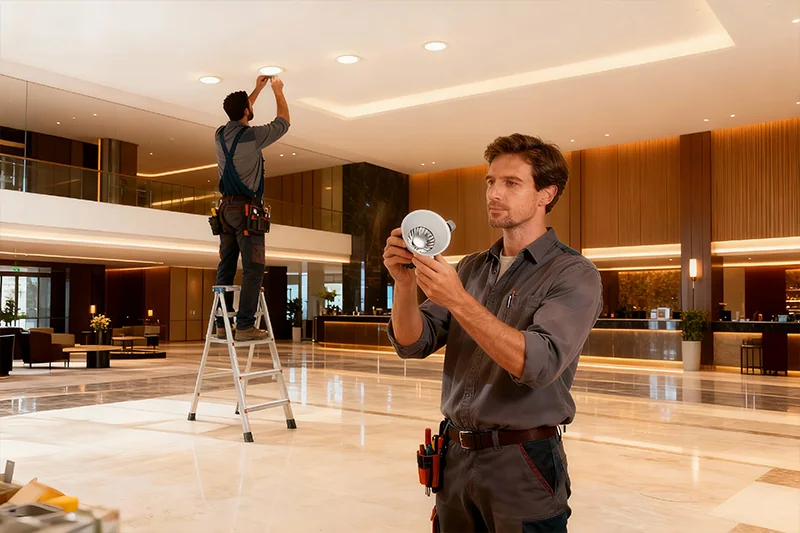
Modular installation of ceiling downlights supports quick maintenance, creating a bright and welcoming reception space that enhances first impressions and reinforces the brand's high-end image.
Explore More Solutions
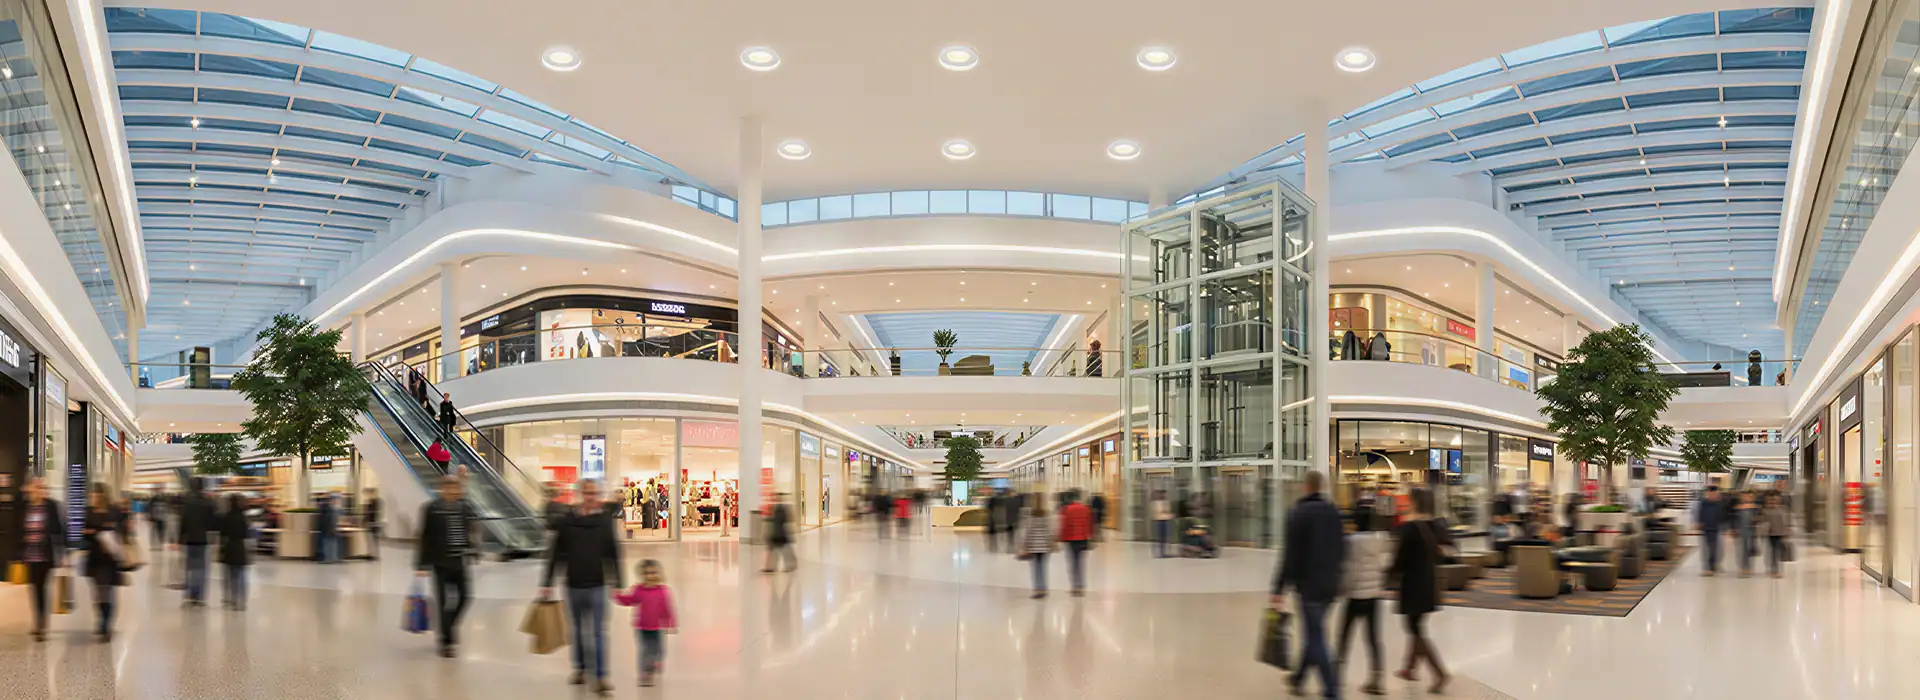
Shopping Mall Lighting Solutions
Evenly distributed light from ceiling downlights, combined with waterproof and durable features, creates a vibrant and spacious public area, attracting foot traffic and improving overall shopping comfort.
Explore More Solutions
ANOVA focuses on providing you with lighting solutions.

As a professional lighting importer
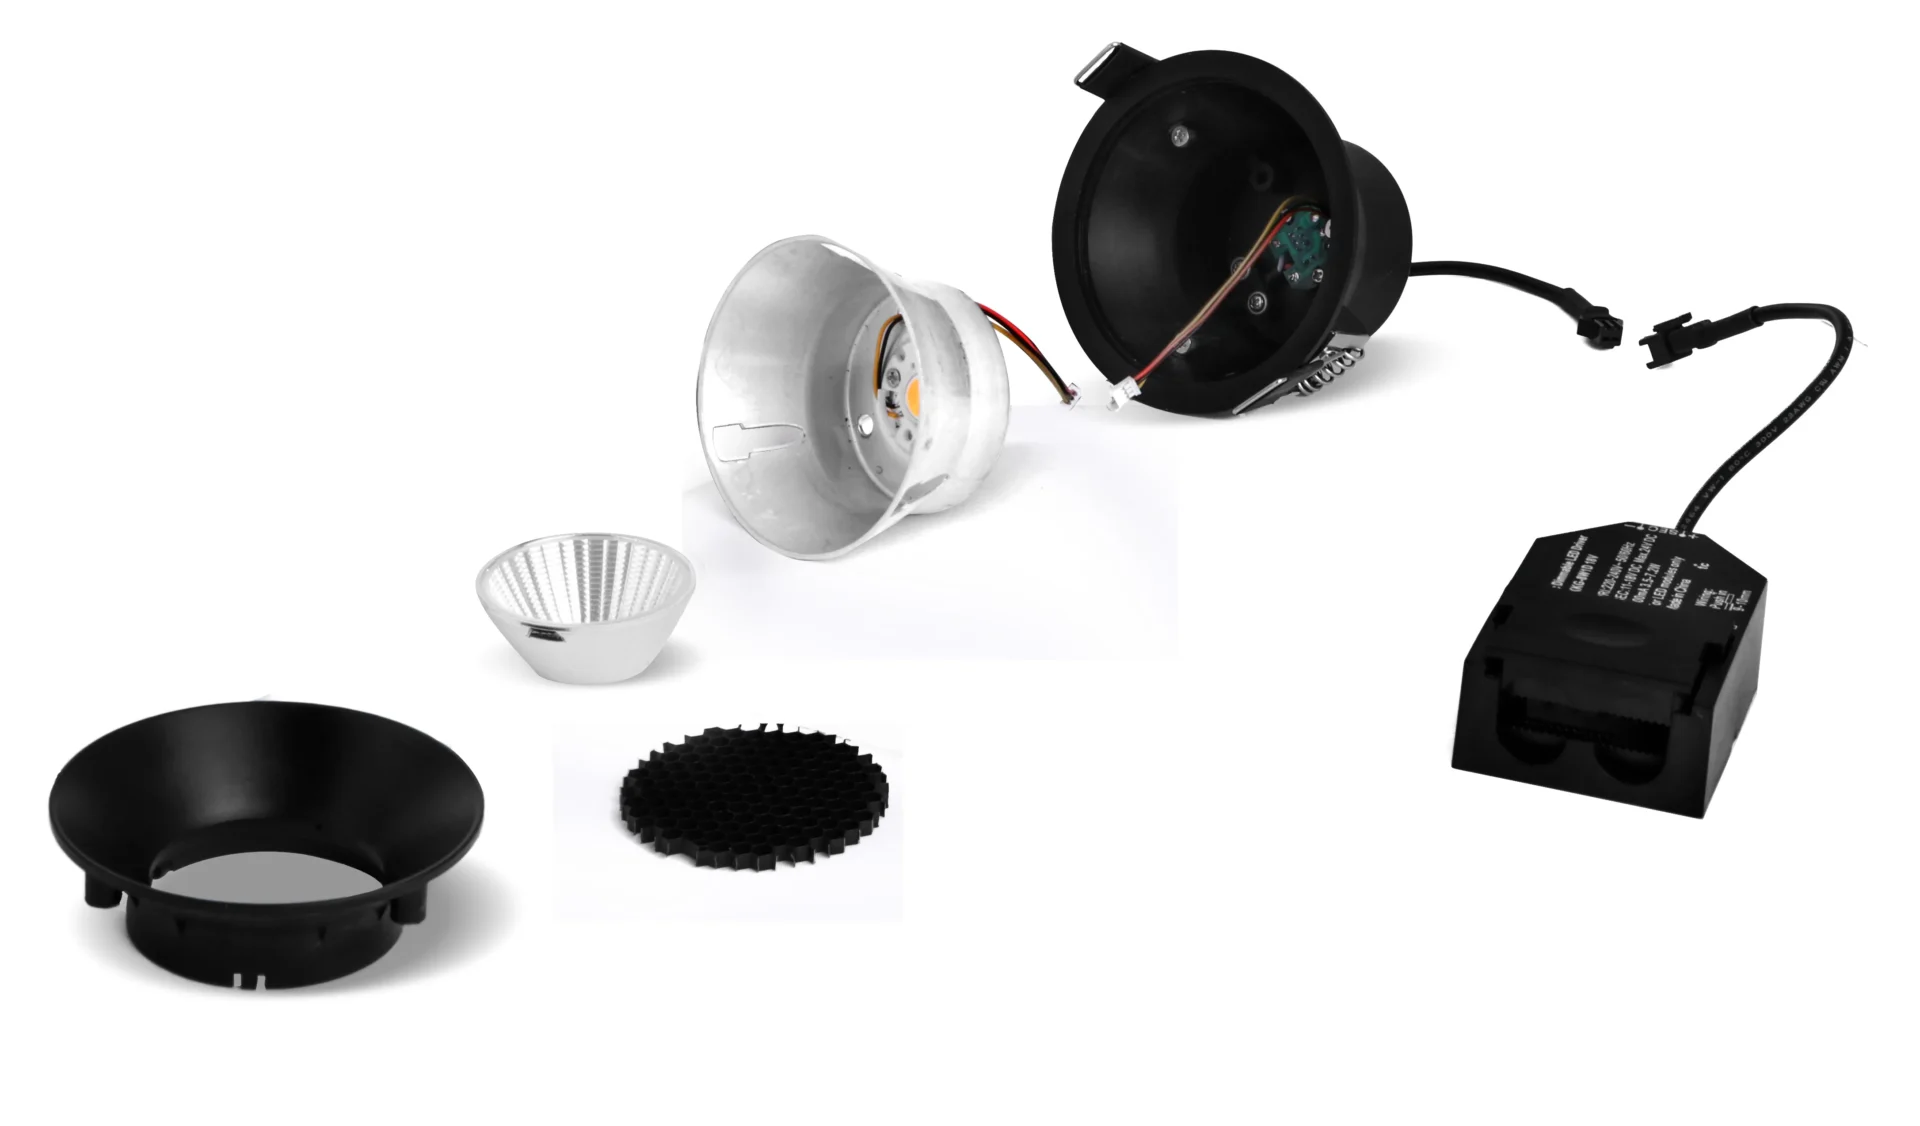
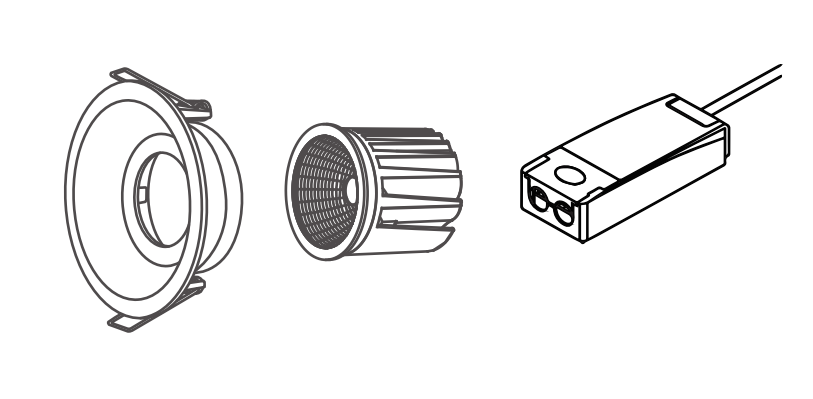
Our modular design allows you to reduce inventory and achieve higher net profits.
As a Contractor
Our modular design can help you reduce inventory and achieve higher net profits.
As a lighting designer
Our products, with CRI > 98 and TM-30 Rg (Gamut) 95-105, deliver museum-quality
color reproduction.
How to Choose a Truly High-Value Lighting Solution?
With Superior Environmental Protection, light sources are ensured lasting stability, fundamentally eliminating these hidden dangers and securing long-term project benefits.
High Maintenance Costs?
High-grade protection reduces failures at the source, ensuring business stability.
Safety Risks?
Our fully sealed design provides the highest level of safety and risk avoidance.
Low ROI?
Durable materials ensure long-term performance and deliver true long-term investment value.
Low Operational Efficiency?
Our low-maintenance design simplifies operations, freeing up your team for core business tasks.
Your Solution in the Making
More Than Production,We Engineer Your Success
At ANOVA LIGHTING, we believe in the power of tailored solutions. Backed by advanced manufacturing infrastructure and rigorous R&D, we don’t just produce lights—we engineer dedicated lighting solutions designed to elevate your business.
ABOUT US
As the new century dawned, the LED lighting industry began to experience a transformative shift, characterized by its distinctive design trends. In the year 2003, Anova emerged with a vision to set the standard in the LED lighting sector. Driven by this ambitious goal, Anova embarked on the development and manufacture of lighting solutions tailored for residential spaces. Our design philosophy is defined by the pursuit of optimal lighting quality and timeless aesthetics, ensuring enduring functionality. Since its inception, Anova has been a trailblazer in shaping the design and advancement of LED lighting, a role it is committed to fulfilling in the years to come.
Years
0
OEM /ODM Experience
Days
0
0
Customized Solution
0
Years Warranty
0
+
Patented Products
In-House R&D, Production & Quality Assurance
High-Pressure Water Jet Testing (IP Rating)
This test ensures the product meets international IP waterproof standards, guaranteeing the long-term reliability of the luminaire in wet or harsh environments, preventing electrical failures and corrosion problems.
Integrating Sphere and Spectroscopic Analysis
Through integrating sphere and spectroscopic analysis, we ensure that the luminaires provide stable lighting performance in practical applications.
Material Performance Testing
We identify how materials perform under extreme conditions, ensuring that components do not affect overall structural integrity due to aging or deformation.
Product Aging Testing
Through accelerated aging processes, we can test the stability of luminaires in high-temperature and high-humidity environments to ensure they maintain high performance after installation and reduce maintenance costs.
Product Development Team
With the professional guidance of our R&D team, we can optimize the functionality and compatibility of our products, ensuring that each luminaire has a competitive advantage in the market and meets diverse application needs.
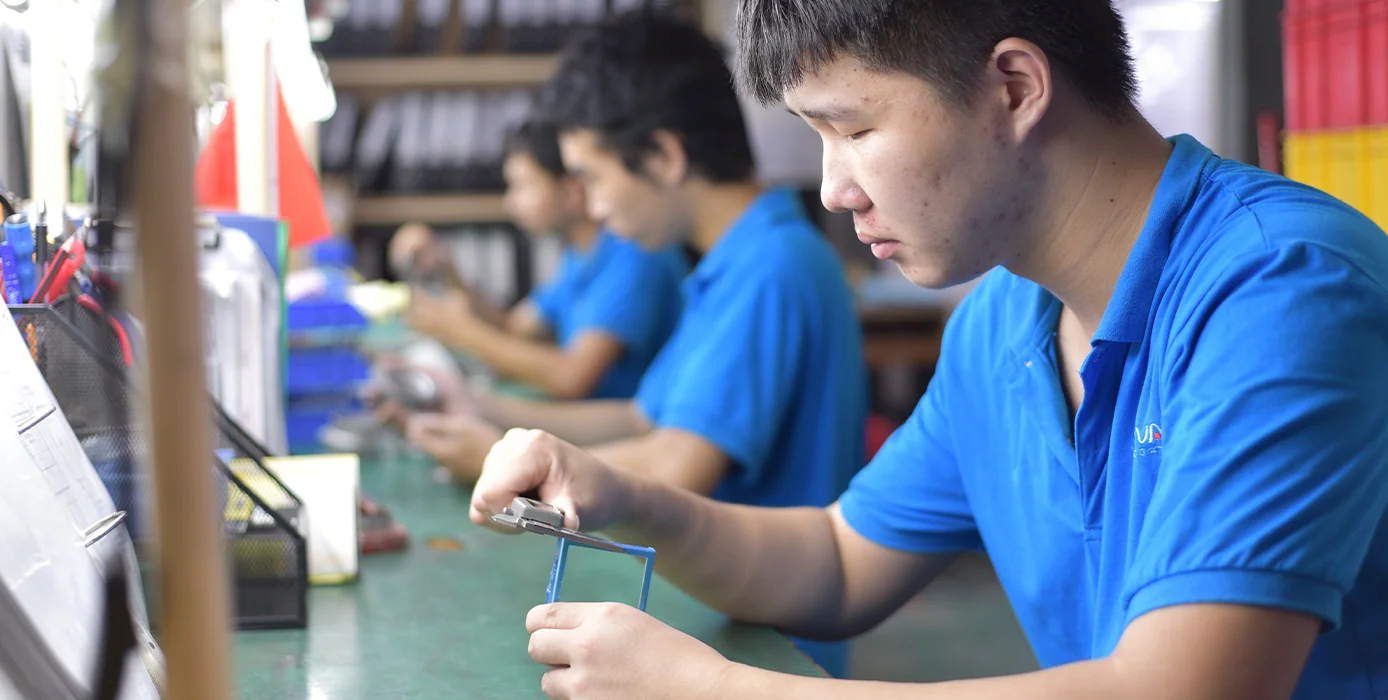
Production Line
Through production line monitoring, we can detect deviations in the production process, ensuring that each product meets precise specifications.
Voltage Testing
Through voltage testing, we can verify the circuit's response under fluctuating voltage, ensuring that the lighting fixtures are protected from short circuits or burnout risks.
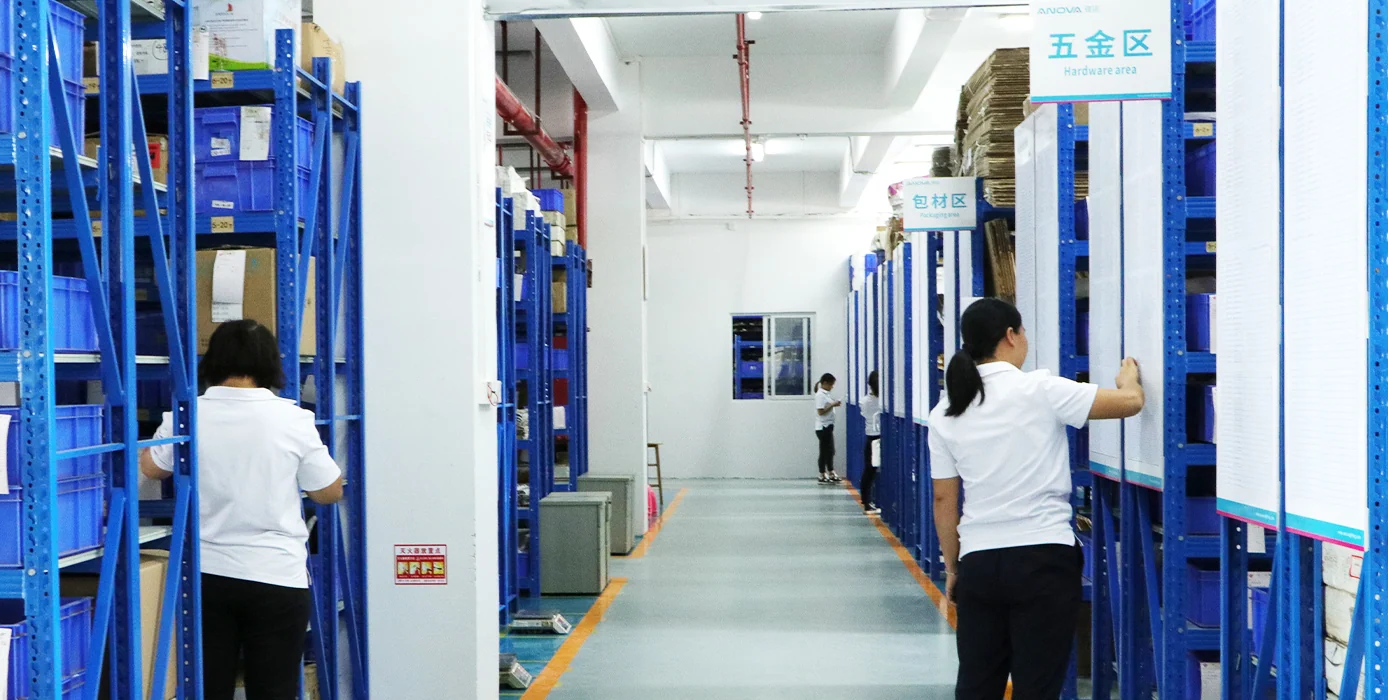
Warehouse and Inventory Management
Implementing efficient logistics standards ensures the integrity of product storage and distribution.


Want To Be the Next Winning Brand?
ANOVA’s one-stop service will give you an absolute competitive advantage.