
For astute lighting importers and distinguished architectural brands, the bedrock of reputation is product consistency. Explore how Anova’s commitment to rigorous 3-step MacAdam Ellipse binning, ISO-certified quality assurance, and advanced R&D guarantees the uniform, high-caliber illumination required for high-stakes commercial projects.
Introduction: The Silent Liability Threatening Brand Integrity
In high-end hospitality and architectural design, technical consistency is the primary currency of credibility. A single project with mismatched color temperatures can undermine years of brand building. Consider a luxury hotel where downlights project varying tints—some clean white, others with subtle pink or green undertones. This chromatic fluctuation, often called the “rainbow effect,” is more than an aesthetic flaw; it is a significant risk factor that leads to project rejections and costly warranty claims.
For importers and specialized distributors, the difference between a premium specification-grade product and a reputational liability is determined by two often-overlooked manufacturing rigors: precise LED binning and uncompromised Quality Control (QC). At Anova, we recognize that our partners’ profitability depends on component reliability. This analysis examines why chromatic consistency and laboratory validation are non-negotiable for brands aiming to lead the competitive lighting market.
Decoding LED Binning: The Technical Science of Chromatic Uniformity
“3000K Warm White” is not a static metric; it is a baseline with significant potential for manufacturing variance. LED semiconductor production is inherently variable; without a sophisticated sorting process—known as binning—a single batch can exhibit deviations in color, luminous flux, and forward voltage.
The Imperative of MacAdam Ellipses and SDCM Standards
The industry benchmark for quantifying these variations is the MacAdam Ellipse, measured via the Standard Deviation of Color Matching (SDCM).
- 1-Step to 3-Step: The color difference is virtually imperceptible to the human eye, ensuring a seamless visual experience across large installations.
- 5-Step or Greater: Variations become visible, resulting in the inconsistent “rainbow effect” that triggers architect complaints.
For prestigious applications—museums, galleries, and luxury retail—a 3-step MacAdam Ellipse is mandatory. Anova implements rigorous binning protocols to guarantee that every module, whether installed today or as a replacement years later, maintains identical chromaticity. This precision ensures that importers can bid on high-margin specification-grade projects with total confidence.
Beyond Chromaticity: The Necessity of Flux and Voltage Binning
Consistency must extend to luminous flux and forward voltage. When a contractor installs fifty downlights in a boardroom, every unit must share similar specifications. This uniformity is critical for compatibility with sophisticated dimming systems and ensuring uniform brightness across the ceiling plane.
Behind the Scenes: How Integrated R&D and Lab Testing Underpin Reliability

Standards are only as effective as the testing behind them. At Anova, Quality Control is not a final checkbox but a scientific methodology embedded throughout the production lifecycle. Our investment in a state-of-the-art Lighting Lab allows us to validate technical data before production begins, transforming us from a supplier into a strategic manufacturing partner.
The Four-Step Quality Assurance Framework (ISO 9001:2015)
Our system is designed to intercept defects at every stage:
- Raw Material Inspection: Strategic partnerships with CREE, Bridgelux, and PHILIPS ensure high-quality components from the start.
- Semi-Finished Product Verification: Active monitoring during assembly prevents errors from compounding.
- LED Component Evaluation: Independent testing of light sources verifies performance data against chip-maker claims.
- Final Product Validation: 100% operational checks on finished units ensure out-of-the-box functionality.
Simulations for Real-World Durability
We replace theoretical data with empirical evidence:
- Photometric Verification: Using advanced goniophotometers, we ensure a 24° beam angle is exactly 24°—precision that lighting designers require for accurate lux level calculations.
- Thermal Management: We test our die-cast aluminum heat sinks to ensure they effectively dissipate energy, preventing premature lumen depreciation.
- Environmental Resilience: Our IP65 models undergo salt spray and water resistance testing, protecting your brand from corrosion-related failures in coastal or high-moisture environments.
Beyond ensuring the longevity of individual products, our R&D approach extends to creating systemic solutions that drive operational efficiency for our partners.
The Business Solution: Modular Precision for Inventory Efficiency
Wholesalers and distributors often struggle to balance lean inventory with project versatility. Stocking thousands of unique finished fixtures is capital-intensive. The Anova MR16 LED Module Series resolves this logistical challenge through modular engineering.
The Strategic Advantage of Modularity for Distributors and Contractors
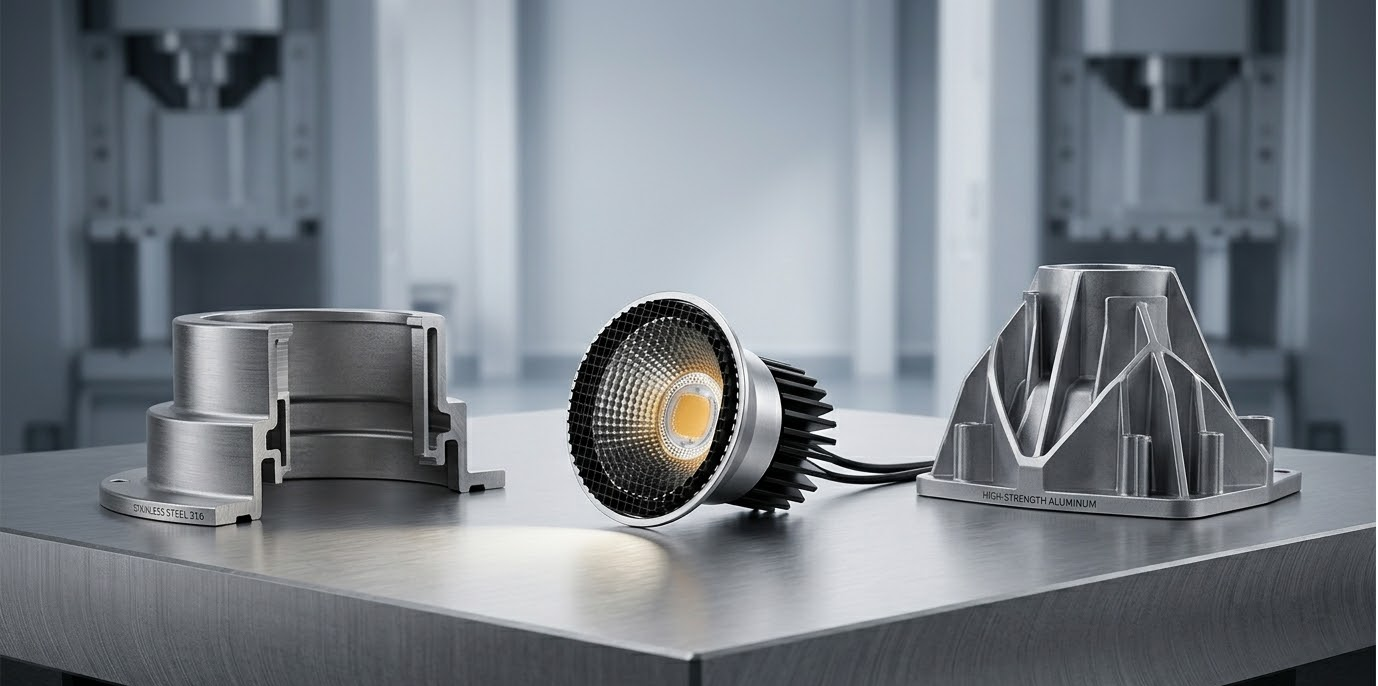
The Anova MR16 Module series ingeniously separates the light engine from the trim.
- For Distributors: Stock a single category of high-performance modules and pair them with various housing styles (round, square, anti-glare). This improves cash flow and reduces warehouse overhead by lowering SKU complexity.
- For Contractors: Maintenance is simplified. Modules can be exchanged from the front without disturbing the ceiling infrastructure or plaster frames, reducing labor costs.
Ready to optimize your inventory? [Request a Sample Kit] to see our modular system in action.
Product Spotlight: Precision Engineered for Market Excellence
Our product portfolio demonstrates how deep QC and R&D translate into market-leading features:
- 10W Tunable White MR16 Module (VB5070TWL):Engineered for exceptional versatility, this module empowers distributors to satisfy diverse project requirements—from hospitality to office environments—using a single, highly adaptable SKU. It provides a Tunable White range of 2700K-6500K, enabling a seamless transition from warm, comforting tones to crisp, illuminating white. With a CRI of over 90, colors remain accurate for retail displays or artwork. Additionally, its IP65 rating allows for damp location installation, maximizing inventory turnover by covering multiple application scenarios with one product.
- High Efficiency 150lm/W Series: Energy efficiency constitutes a primary concern for modern building codes (such as ErP). Our high-efficiency modules deliver up to 150 lumens per watt, significantly reducing electricity consumption without sacrificing brightness, serving as a key selling point for eco-conscious developers and LEED-certified projects.
- SunLike Full Spectrum Series: Innovating for human health, our “SunLike” modules are engineered to mimic the natural solar spectrum. By eliminating the blue light spike typically found in traditional LEDs, these modules improve visual comfort and support healt
These modules are designed to integrate perfectly into our sustainable housing, such as those manufactured from Recycled Ocean Plastic, further enhancing the unique selling proposition for brands focusing on environmental sustainability.
Anova: Your Strategic Manufacturing Partner
Since 2003, Foshan-based Anova has evolved from a factory into a global solutions provider. Our 2023 facility relocation has further enhanced our intelligent manufacturing capabilities, serving partners across North America, Europe, and Australia.
- Financial Security: Reduced warranty claims through 3-step binning.
- Operational Agility: 8-hour after-sales response time and robust supply chain resilience.
- Sustainability Leadership: Pioneers in using Recycled Ocean Plastics, allowing our partners to offer products with a compelling environmental narrative.
We invite you to explore our Company Profile and observe how our Milestones reflect a history of continuous improvement and unyielding dedication to the lighting craft.
Conclusion
In a competitive market, the distinction between a commodity and a premium brand lies in the rigor of the manufacturing process. Strict LED binning eliminates the commercial risk of color inconsistency, while comprehensive lab testing ensures that performance in the ceiling matches the data on the spec sheet.
By partnering with Anova, you gain a supply chain built on precision and reliability. Whether through modular solutions that maximize your sales flexibility or lab-tested quality that secures your reputation, we are dedicated to your long-term business growth.
Ready to elevate your product line with precision-engineered LED solutions?
Explore Technical Specification & IES Files
FAQs
Q: How does Anova’s binning benefit architects?
A: We adhere strictly to 3-step MacAdam Ellipse binning. This ensures identical color temperature across all fixtures, eliminating the “rainbow effect” and preserving the architectural intent of the space.
Q: Are these modules suitable for coastal environments?
A: Yes. Our IP65 modules undergo rigorous salt spray and waterproof testing in our Lighting Lab, ensuring reliable performance in humid or coastal areas.
Q: How does the modular design lower inventory risk?
A: Instead of stocking 100 variations of finished lights, you stock core modules and interchangeable trims. This allows you to assemble Round/Square, Black/White, or IP20/IP65 combinations on demand, significantly reducing tied-up capital.